GRAVITY DIE CASTING
Fine surfaces and tight tolerances for stable volume production
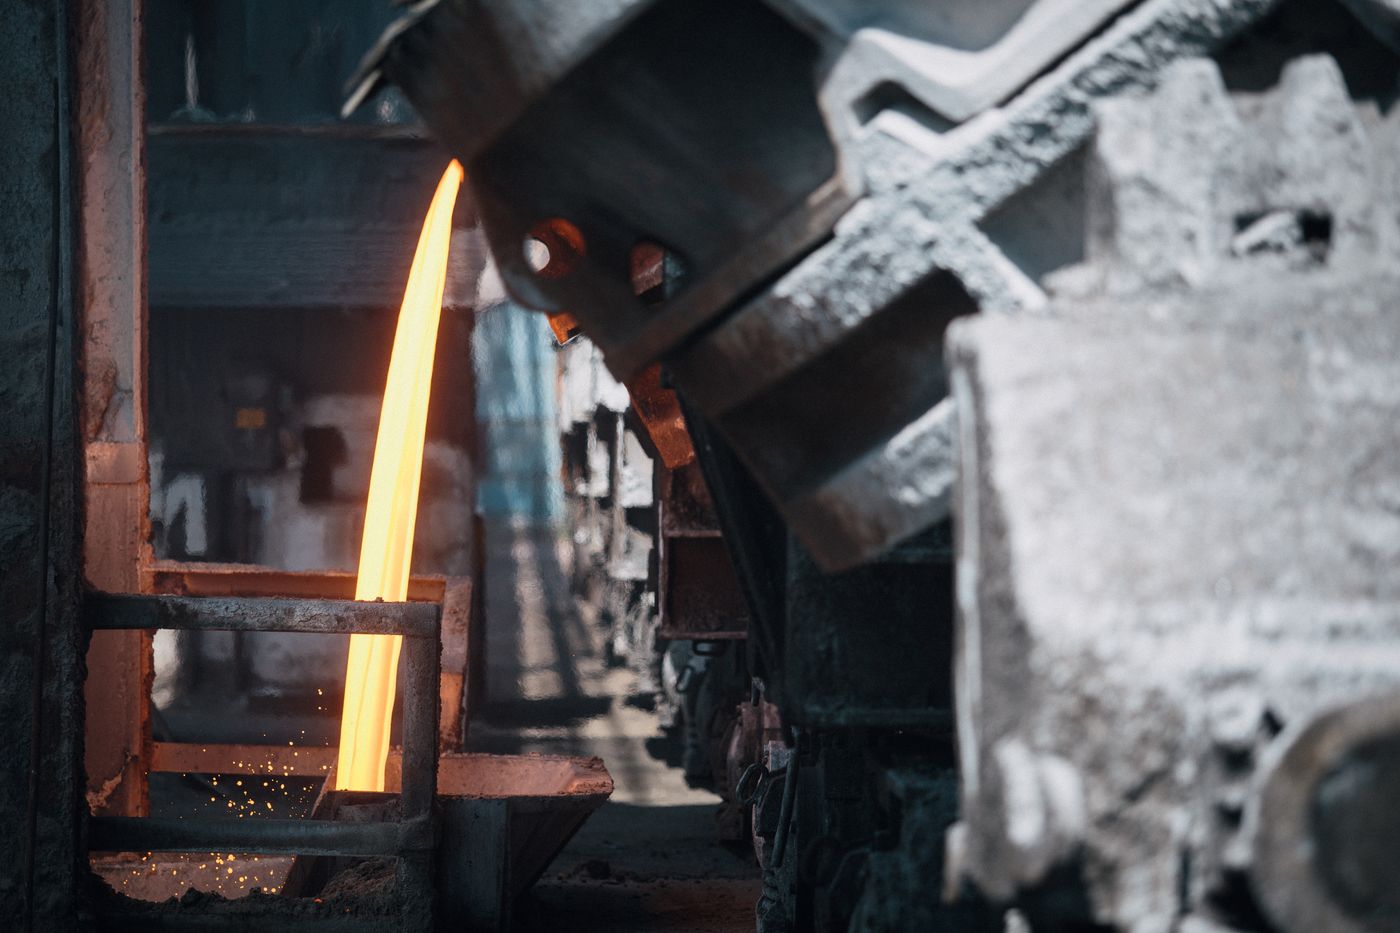
In gravity die casting, molten metal is poured into a metal mold using gravity alone. Rapid cooling produces a dense structure with higher strength, accuracy and surface quality than sand casting.
Our tilt-pour machines control the flow gently, keeping entrapment defects to a minimum.
FEATURES
Key Features
-
01
High strength and pressure tightness
Dense structure and T6 heat treatment suit hydraulic and pneumatic parts that must withstand pressure.
-
02
Near-net shapes, less machining
Low dimensional variation minimizes machining allowance, cutting downstream cost and material loss.
-
03
Die design and maintenance in-house
We design, modify and maintain our own dies, keeping quality consistent through long production runs.
SPECIFICATIONS
Capabilities
| Alloys | AC2B / AC4C / AC4CH / AC7A, etc. |
|---|---|
| Part size | Up to 600 × 600 × 400 mm |
| Part weight | 0.1 – 40 kg |
| Lot size | 100 – 10,000 pcs / month |
| Tolerance | Equivalent to JIS B 0403 CT6 – CT8 |
| Heat treatment | T5 / T6 / T7 (in-house) |
| Secondary processes | Machining / impregnation / leak testing / shot blasting |
PROCESS
Production Process
- 01
Die design & CAE
Dies and gating are designed with both part geometry and productivity in mind.
- 02
Preheating & coating
Dies are preheated and coated for release and smooth metal flow.
- 03
Melting & degassing
Hydrogen is removed from the melt to eliminate the cause of porosity.
- 04
Tilt pouring
The die is tilted while pouring to prevent air entrapment.
- 05
T6 heat treatment
Solution and aging treatment provide the required strength and hardness.
- 06
Machining & inspection
Parts are machined, leak-tested and dimensionally inspected before shipment.
PRODUCTS
Product Examples
Joint hub for industrial robots
Heat sink for inverters
End cover for motors
Manifold for pneumatic equipment
* Product photos will be replaced after the photo shoot (illustrations are used in this demo).